Silicone Sealant for Stainless Steel and Metal Fabrication
Stainless steel and other non-porous metals resist primerless adhesion more than almost any other substrate. Add the requirement that the sealant must not attack passivated surfaces, coatings or weld lines, and the choice narrows considerably.
Why Metal Fabrication Is Hard on Sealants
Non-porous, smooth and often chemically passivated — stainless steel gives a sealant very little to grip, and the wrong chemistry will attack the surface it is meant to protect.
- Non-Porous Surface: Stainless steel offers no mechanical key, so adhesion depends entirely on chemical bonding — a formulation without the right adhesion promoters will peel at the edges.
- Acid Attack on Passivated Surfaces: Acetoxy cure sealants release acetic acid, which can attack the passive chromium oxide layer and leave a discolored or etched mark.
- Thermal Movement in Long Runs: Fabricated metal sections are often long and continuous, producing significant thermal movement that the joint must absorb without stressing the bond line.
How PIROI Solves It
Modified adhesion promoter package that grips stainless steel, anodized aluminium and galvanized surfaces without a primer step, in a neutral cure chemistry that leaves the surface untouched.
- Primerless Metal Adhesion: Modified adhesion promoters grip stainless steel, anodized aluminium and galvanized steel without a primer step.
- Non-Corrosive Chemistry: No acid byproducts — passivated surfaces, coatings and weld lines are unaffected during cure.
- Movement Capability: Class 25 and Class 50 options for long fabricated runs and high-thermal-movement sections.
- Stainless steel sealants — acid cure is out: acetoxy sealants release acetic acid, which attacks the passive chromium oxide layer that makes stainless steel stainless. The result is pitting or staining along the bond line, visible within months. Neutral cure is mandatory, and surface finish matters: brushed, polished and 2B mill finishes each behave differently, with polished surfaces needing cleaning and often a primer.
- Adhesion on stainless steel sealants: the usual cause of failure is not the product but contamination — fabrication oil, polishing compound and workshop dust sit invisibly on the surface. A solvent wipe before sealing belongs in the method statement, and an adhesion test on an offcut of your actual finish is worth more than any datasheet figure measured on a generic plate.
- Related technical guides: structural vs weatherseal silicone sealant, silicone sealant joint failure modes repair, chinese vs astm sealant standards test report — each covers the engineering behind the grade you are specifying.
Stainless steel gives a sealant almost nothing to grip: it is smooth, non-porous and often chemically passivated, so adhesion depends entirely on the formulation. Run a trial adhesion test on the actual surface finish used on the project, including the weld areas, before sealing production parts.
Stainless Steel & Metal Fabrication — Critical Engineering Parameters
Primerless Metal Adhesion
Grips stainless steel, anodized aluminium and galvanized steel without a primer step.
No Surface Attack
Neutral cure — no acetic acid to attack passivated surfaces, powder coatings or weld lines.
Long Run Movement
Class 25 / 50 options for long continuous fabricated sections with significant thermal movement.
Clean Aesthetics
Non-staining, does not bleed onto visible metal surfaces around the joint line.
Sealants for Stainless Steel & Metal Fabrication
 Specialty
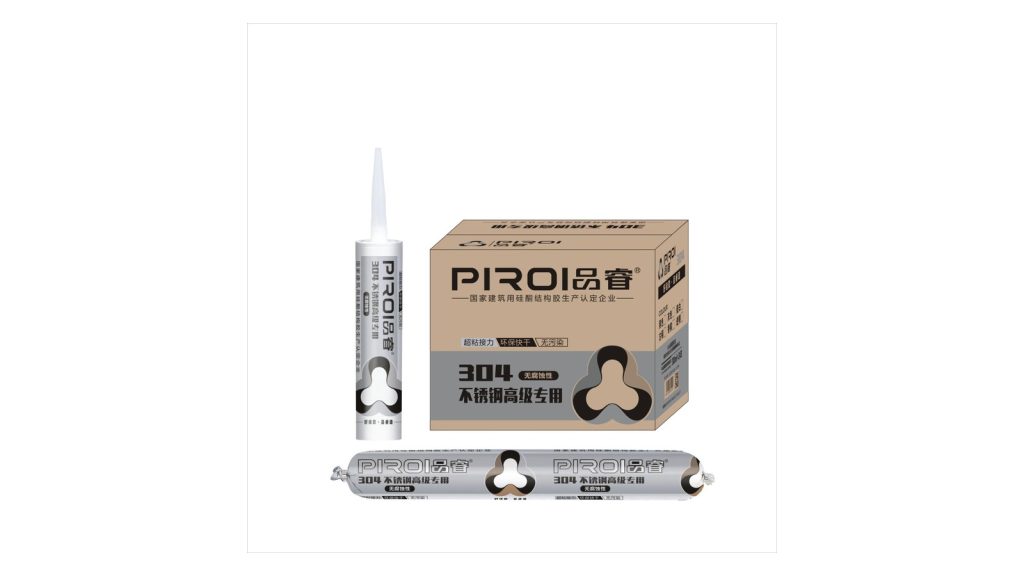
Stainless Steel Silicone Sealant
Specialized sealant for stainless steel surfaces. Non-corrosive formula, excellent adhesion, ideal for stainless steel kitchen and sanitary applications.
View DetailsMOQ, Lead Time & Private Label
Installation Protocol for Stainless Steel & Metal Fabrication
Degrease
Remove cutting oil, protective film residue and handling oils with isopropanol. Metal surfaces are usually contaminated from fabrication.
Confirm Surface Finish
Identify whether the surface is mill finish, brushed, polished or coated. Coated surfaces may require a different preparation.
Trial Adhesion Test
Run a peel test on an offcut. Metal adhesion depends heavily on surface condition and alloy, so verify before full application.
Apply Sealant
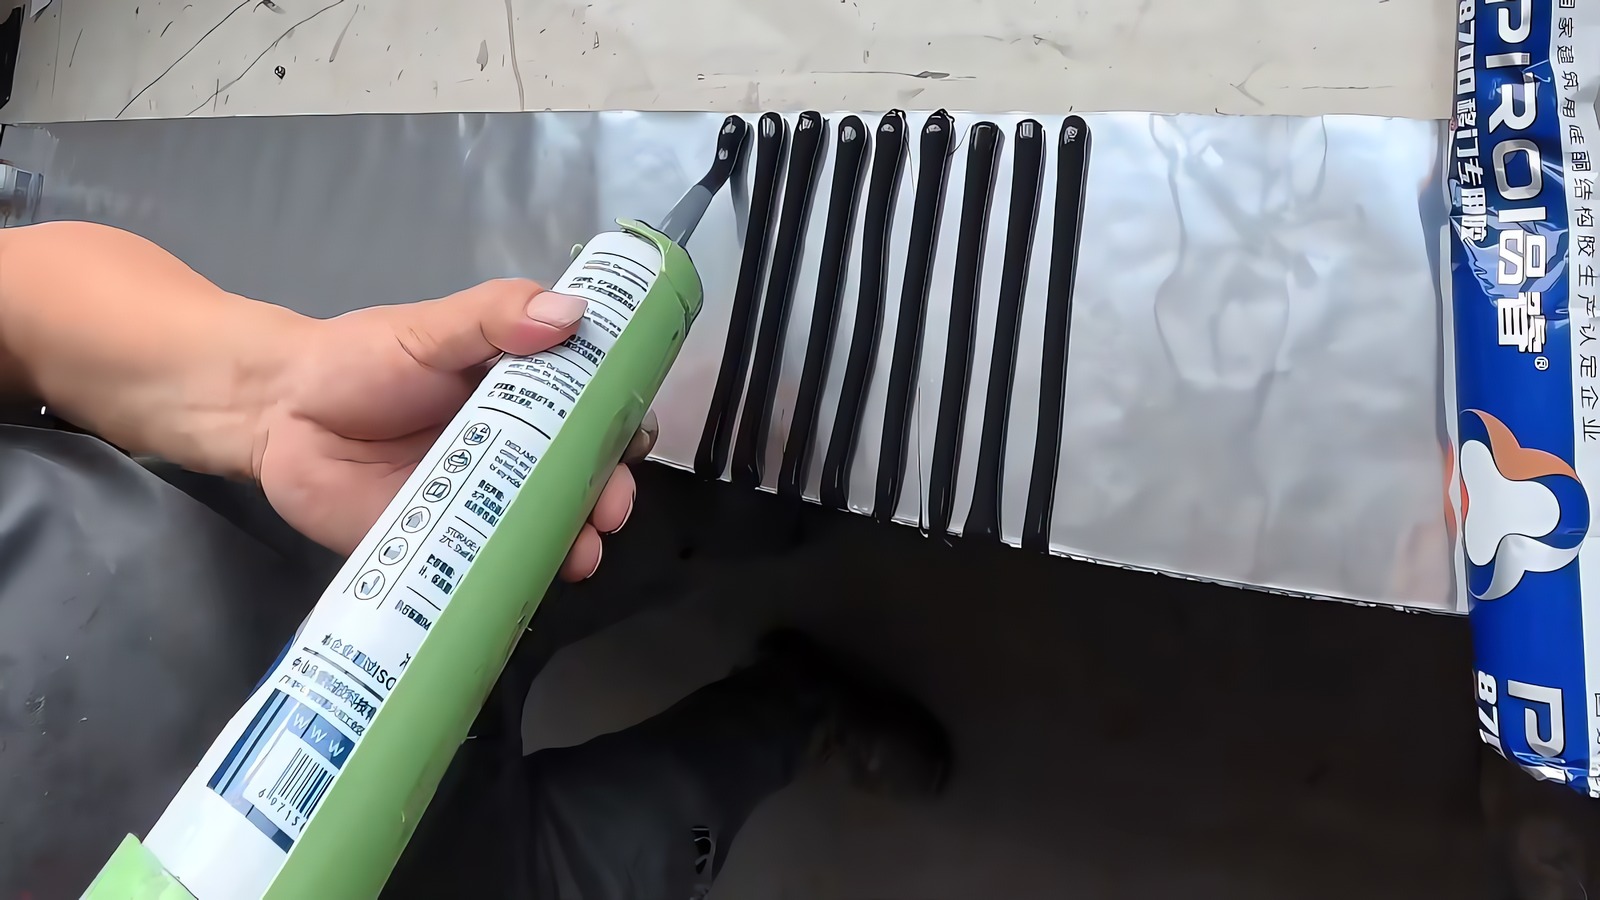
Apply in a continuous bead with positive pressure. Tool immediately to wet out both bond faces.
Cure
Allow full cure before the assembly is moved or exposed to load. Do not pressure-wash during cure.
FAQs — Stainless Steel & Metal Fabrication
Why is stainless steel harder to bond than other metals?
It is non-porous and smooth, so there is no mechanical key for the sealant to grip. Adhesion depends entirely on chemical bonding, which means the formulation has to be matched to the surface.
Will the sealant attack the passivated surface?
Not with our neutral cure products. Acetoxy sealants release acetic acid, which can attack the passive chromium oxide layer, so they are not suitable for passivated stainless steel.
Do we need a primer?
Our metal-compatible products are primerless, but the surface must be degreased first. Oil, cutting fluid and handling residue are the usual cause of adhesion failure on fabricated metal.
Long fabricated runs move a lot in the sun — will the joint hold?
That is a joint design question rather than a sealant question. Long continuous runs need the joint sized for the full thermal movement of the section, and we offer Class 25 and Class 50 products to match the calculated demand.
Can we test before committing to a full order?
Yes. Send us a sample of the actual material and finish, and we will run an adhesion test and report the result before you order production quantities.
Is there a structural steel sealant in your range?
Structural bonding on steel is an engineered application and is not interchangeable with a general weatherseal, so send us the joint detail before ordering. What we do supply is the neutral cure range that bonds to fabricated steel without releasing acid that could attack the passive layer — PR-999 where a structural grade to GB 16776-2025 is specified. We will run an adhesion test on your actual steel sample first.
What should I use for metal-to-metal sealing joints?
For metal, the issue is that the surface is non-porous and smooth, so there is no mechanical key — adhesion depends entirely on chemical bonding. Our neutral cure products are primerless, but the surface must be degreased first: oil, cutting fluid and handling residue are the usual cause of failure on fabricated metal. Send us a sample and we will test adhesion before you order production quantities.
Can silicone be used for steel sections as well as stainless steel?
Not with the same expectation. Austenitic stainless steel carries a passive chromium oxide layer that acetoxy products can attack, so only neutral cure is suitable there. Mild steel is usually coated, so adhesion depends on the actual coating. Our neutral cure range is primerless on both once degreased. Send us the material and finish and we will report the adhesion result.
Do you supply sealant for metal roofing sheets and flashings?
Yes, a neutral cure weatherseal grade is the right choice for metal roofing laps, flashings and penetrations — it absorbs the thermal movement of long sheet runs and will not etch zinc, aluminium or coated steel. Long continuous runs need the joint sized for the full thermal movement of the section. Tell us the sheet material, run length and expected temperature swing and we will confirm the grade.
What sealant should be used on stainless steel?
A neutral cure silicone sealant, because acetic acid attacks the passive chromium oxide layer on stainless steel and causes pitting along the bond line. Surface finish also matters — brushed, polished and mill finishes behave differently — and fabrication oil or polishing compound must be removed with a solvent wipe before sealing. Where the joint also sees chlorides, the steel grade and the fixings matter as much as the sealant.
Need pricing or a sample for Stainless Steel & Metal Fabrication?
Tell us your substrate, joint dimensions and target market. We will come back with pricing, sample arrangements and the technical data sheet.
- Free adhesion & staining test on your own substrate sample
- OEM & private label from 1,000 pcs
- Typical lead time 15–25 days